• Home
  • Tech
  • Pets
  • Economy
  • Industry
  • Market
  • Wildlife
  • Economy
  • Industry
  • Market
  • Tech
  • Wildlife
News Online
keep your memories alive
Business

How a 3-Channel Dashcam Connects ADAS and DMS AI: A User-Centric Terminology Guide

by Christine September 14, 2026
written by Christine

Opening: what the driver and fleet manager actually need

Start simple: a driver wants safety; a fleet manager wants repeatable results. That tension shapes every term here. If you manage vehicles, you already use hardware like GPS fleet trackers to know where assets are — now you’re adding vision and intelligence. I’ll keep this focused on what you’ll see on the road, what to ask suppliers, and what to avoid when you mix a 3-channel dashcam with ADAS and DMS AI.

Core terms explained plainly

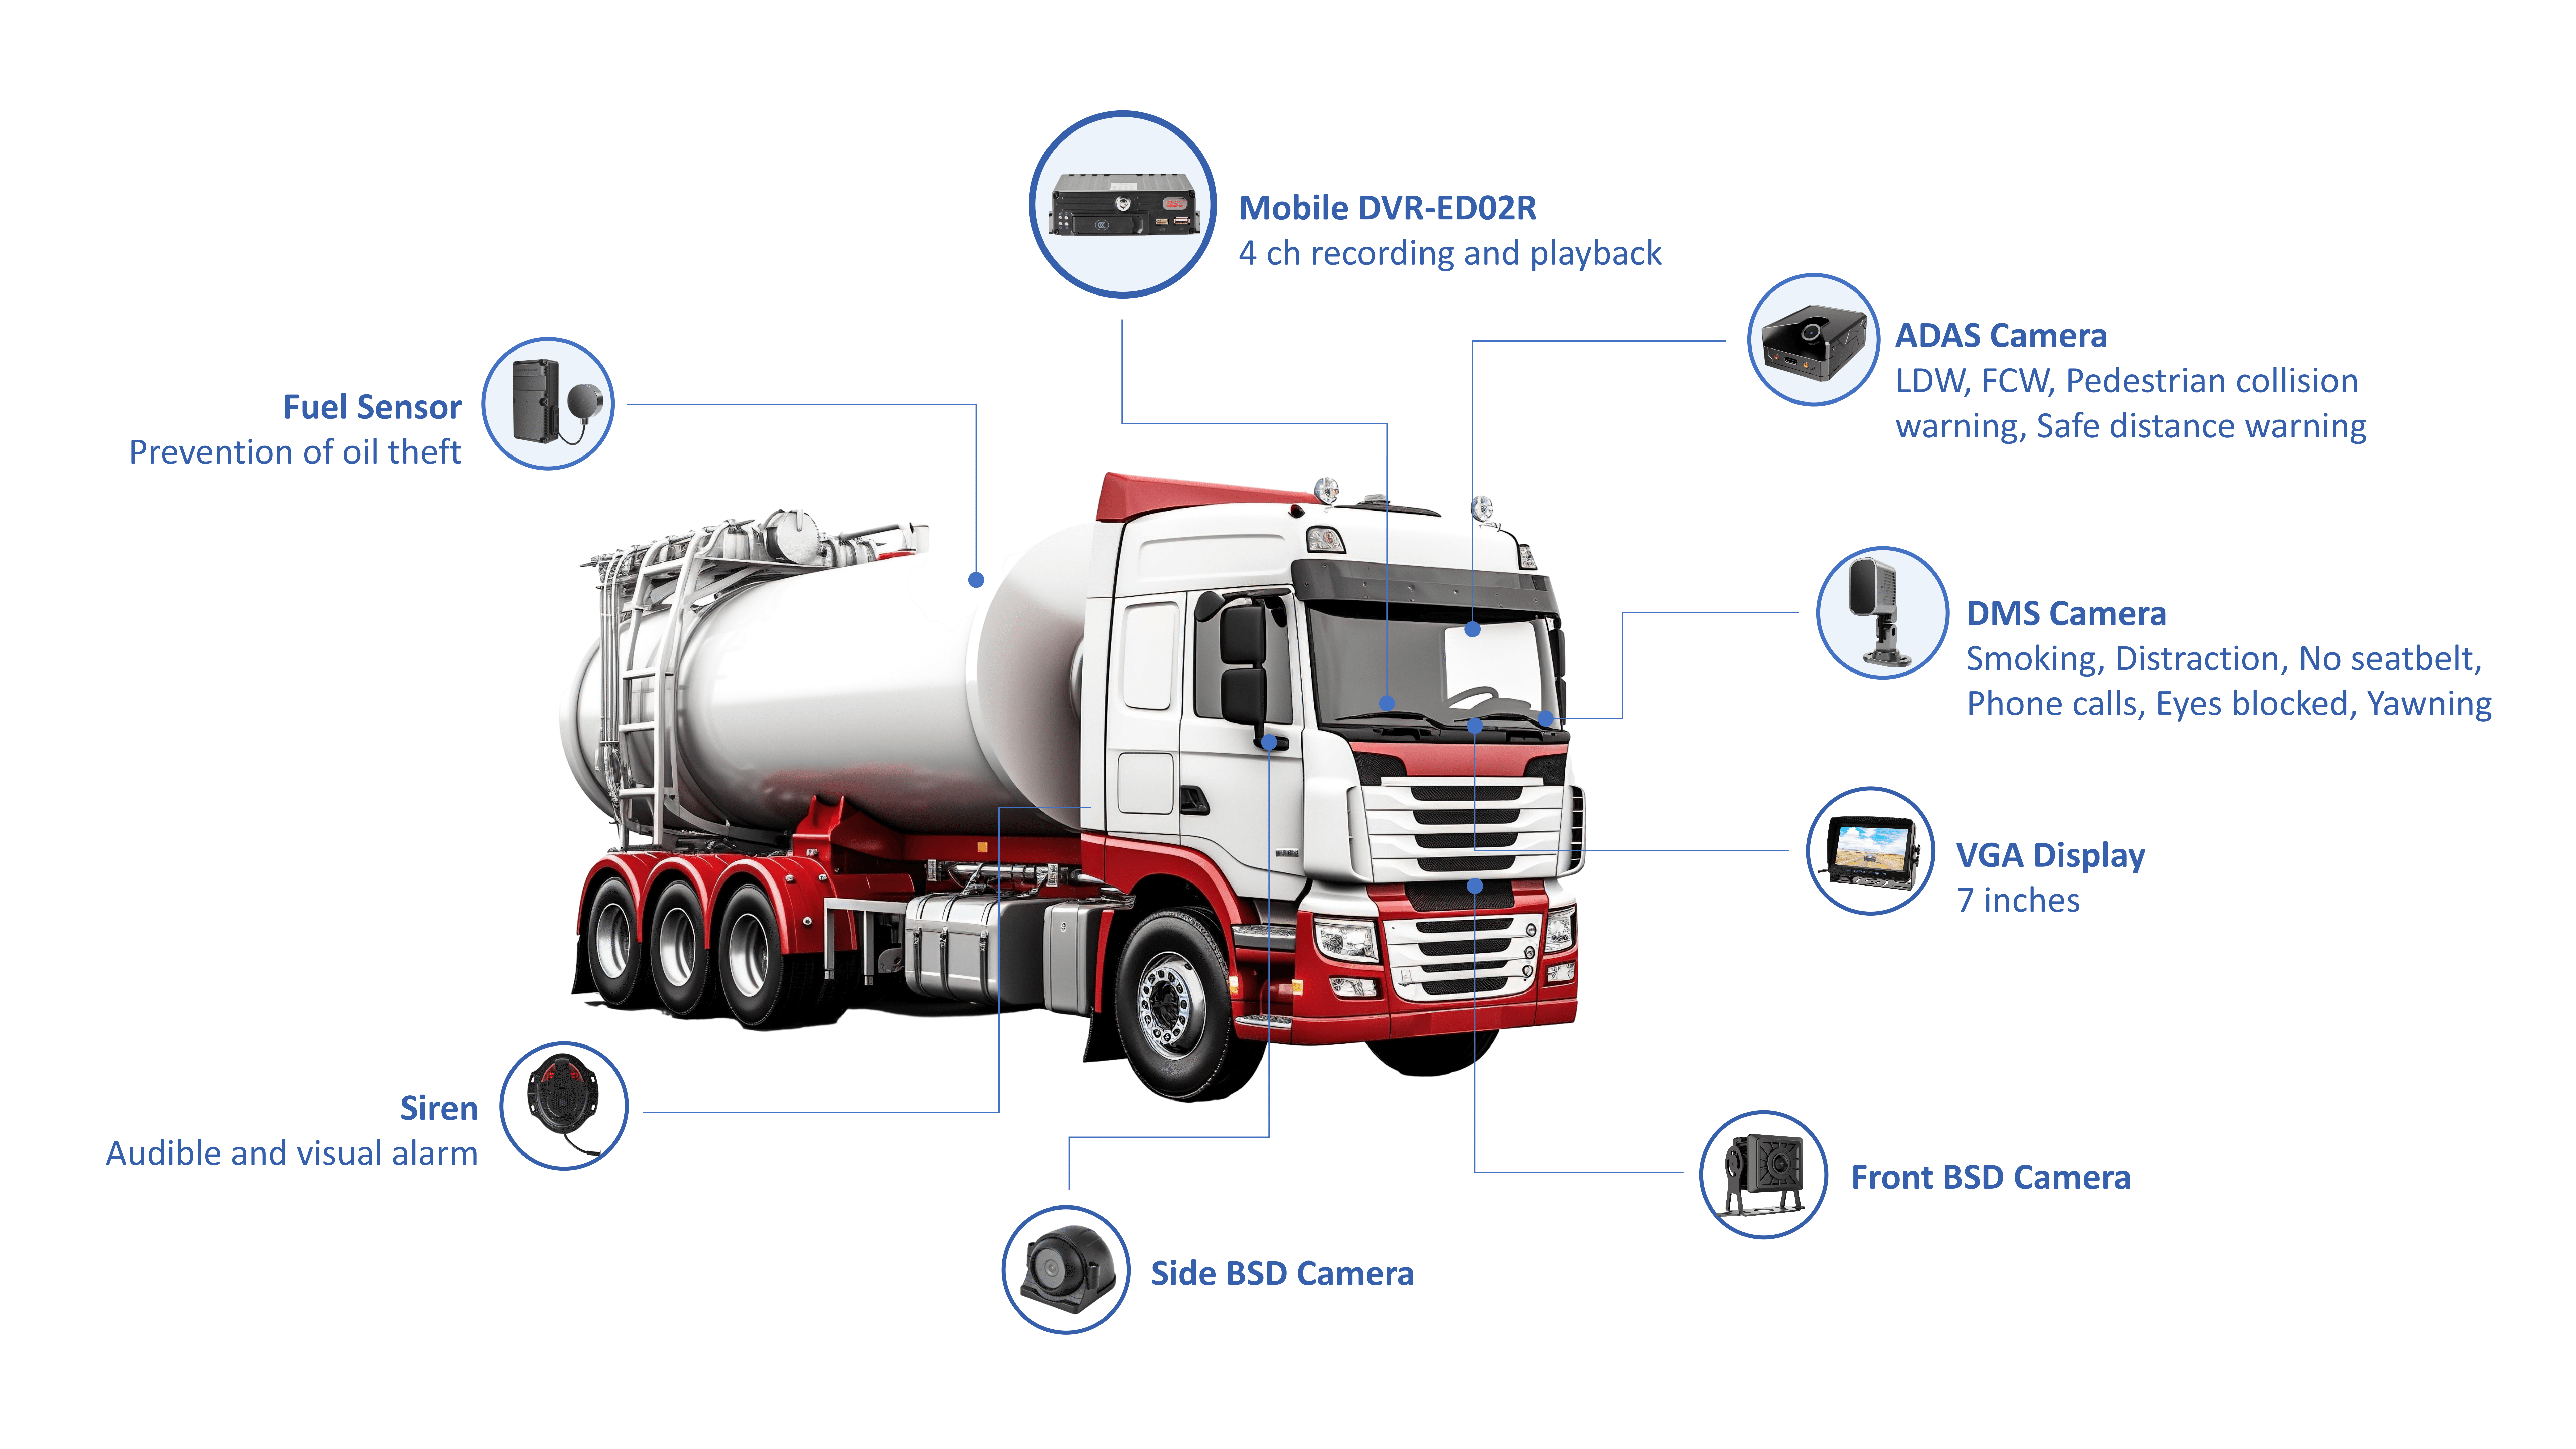
3-channel dashcam — three lenses, usually front, inside, and rear. Front records the road, inside captures driver behavior, rear watches traffic behind. ADAS (Advanced Driver Assistance Systems) — features like lane departure warnings, forward collision alerts, and pedestrian detection; they use the front channel. DMS (Driver Monitoring System) — monitors attention, drowsiness, phone use; relies on the inside channel and AI. AI models — algorithms trained to spot objects, faces, eyelids, and risky actions; they decide when to flag events. Think of them as separate tools that must communicate: one watches the road, one watches the driver, the software ties the story together.

How these systems work together during a shift

Picture a delivery run. The front camera flags a sudden brake; ADAS timestamps and records the risk. The inside camera shows the driver glanced down five seconds before; DMS scores the event as distraction. Telematics and GPS log position and speed. Together you get a causal sequence: hazard, driver state, location. If you already track vehicles with gps trackers for vehicle fleet management, this multi-source record makes incident review faster and less arguable.

User-focused benefits and practical outcomes

Use cases you’ll care about: sharper coaching conversations (video + context); faster insurance claims with time-stamped evidence; targeted retraining when patterns show distracted driving; selective alerts so drivers aren’t overwhelmed. Real-world: a Mexico City municipal fleet reduced repeated risky stops by reviewing combined road and driver footage during weekly coaching sessions. That’s the kind of practical win that matters.

Common setup mistakes to avoid

Misaligned cameras — inside lens pointing too high or blocked by a visor; wrong ADAS sensitivity — too many false positives, drivers ignore alerts; siloed data — dashcam video stored separately from GPS logs, so you lose causal context. Also watch bandwidth and storage: high-res three-channel streams chew data. Prioritize event-based upload, not continuous cloud streaming unless your plan covers it.

How to evaluate suppliers and system combinations

Ask for sample clips from similar vehicles; test detection at night and through sunglasses; insist on synchronized timestamps across dashcams, ADAS logs, and GPS. Compare by these criteria: accuracy of driver attention scoring, latency from event to alert, ease of pulling combined footage, and how the solution handles low-bandwidth uploads. Don’t choose only on price — choose what makes coaching and claims work faster.

Quick checklist for field rollout

1) Camera placement verified with a short road test; 2) ADAS thresholds adjusted by vehicle type; 3) DMS trained or tuned for drivers’ typical headwear and lighting; 4) Event sync checked between video and GPS logs; 5) Data retention policy set so you keep only what you need. Short tests, short fixes. Repeat until drivers accept the system — resistance often drops once false alarms stop.

Final synthesis

When you treat a 3-channel dashcam, ADAS, DMS, and GPS as one toolkit, you get clear incident narratives instead of fragments. That clarity helps coaching, claims, and day-to-day decisions. For fleets that want reliable integration and practical deployment advice, partner selection and setup matter more than flashy specs — and that’s the pragmatic value BSJ brings to real operations.

September 14, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Why Modern Facilities Often Prefer China Genset Manufacturers Over Imported Units

by Cynthia September 13, 2026
written by Cynthia

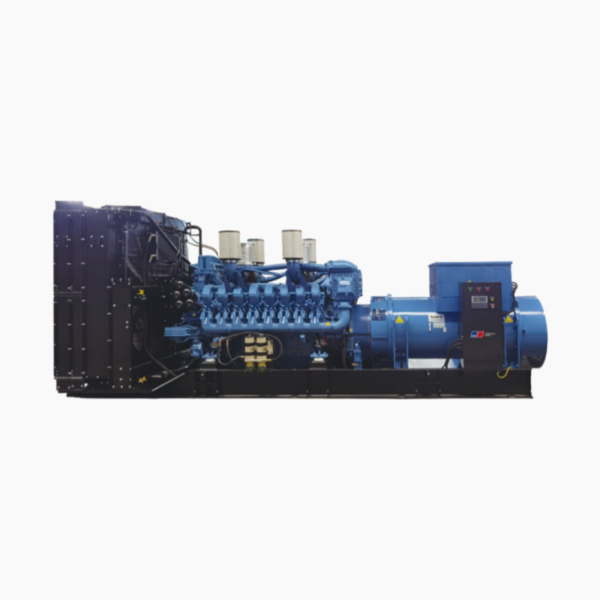
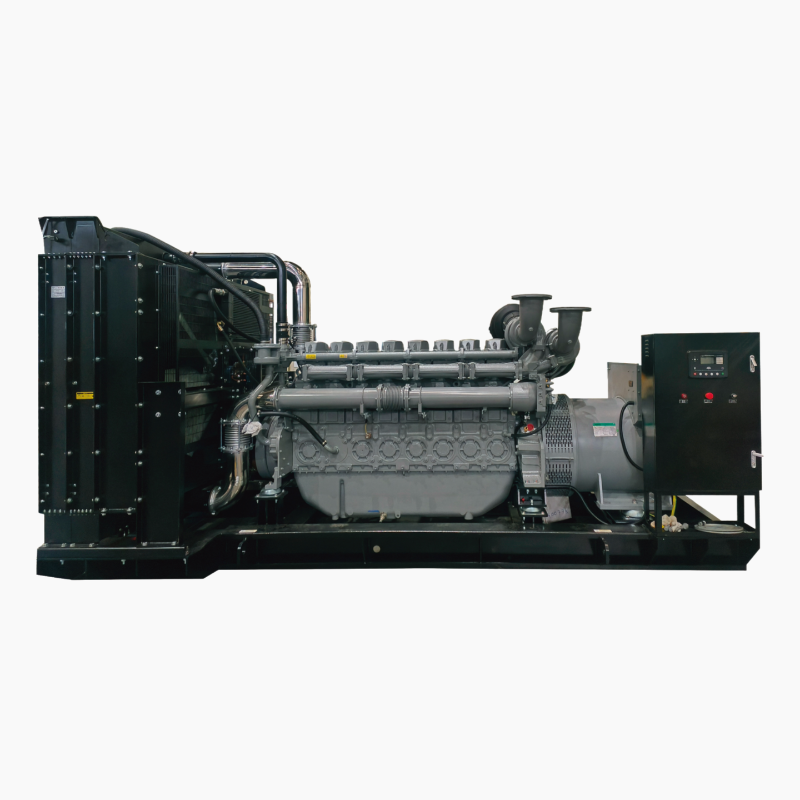
Start with a simple comparison and then follow steps to choose a reliable source. This piece uses a comparative-insight approach and step-by-step clarity to show how a China genset can match or outperform alternatives in cost, serviceability, and technical fit. For a quick reference model, consider the Mtu genset lineup when you benchmark performance and lifecycle cost.

Mtu genset

Step 1 — Map operational needs and emergency scenarios

List the facility’s peak and continuous loads, identify critical circuits, and set acceptable transfer times. Include genset parameters such as kW rating and alternator compatibility so you can size units correctly. Use a simple checklist: peak kW, continuous kW, start-up surge, and critical run duration. This prevents overspecifying an expensive set or undersizing a unit that will cycle too frequently.

Step 2 — Compare technical specs side-by-side

Lay out comparable specs for imported units and China manufacturers: rated power, fuel type (diesel engine vs. gas), fuel consumption at load, emissions tier, and synchronization capability. Pay attention to control systems and aftersales documentation. During an operational production teardown you should capture the {main_keyword} and inspect the {variation_keyword} to confirm tolerances and service access—this exposes real maintenance costs beyond the sticker price.

Step 3 — Weigh total cost of ownership and supply chain realities

Calculate acquisition cost plus scheduled maintenance, spare parts lead time, and typical repair intervals. China manufacturers often offer lower initial cost and nearby parts warehouses; that changes downtime risk calculations. Include vendor responsiveness: a local Mtu genset supplier with stocked spares reduces mean time to repair for campus or industrial sites and can lower buffer inventory needs.

Step 4 — Validate performance with real-world anchors

Reference real events to test assumptions. The 2003 Northeast blackout and subsequent studies showed that fast, correctly sized backup gensets prevented extended outages for many hospitals and data centers. Use that lesson: require vendors to show prior deployments and provide runtime logs or load-bank test records. Look for evidence of routine load-bank testing and documented synchronization trials when parallel operation is expected.

Step 5 — Avoid common procurement mistakes

Avoid buying solely on lowest bid, neglecting alternator matching, or skipping site-specific controls integration. Do not assume every genset module is plug-and-play with your switchgear. Also, beware of incomplete warranties that exclude wear items. Take short factory-acceptance tests and insist on clear spare-parts lists up front — it saves lost production later. —A small upfront test contract often reveals bigger lifecycle differences.

Step 6 — Final comparison checklist

Put the competing offers on a single page: rated kW, fuel consumption at 50% and 75% load, recommended maintenance intervals, spare-parts lead time, warranty scope, and local service network. Include at least one field reference from each vendor. For many facilities the balance shifts toward a China genset manufacturer because of transparent spare availability and lower logistics cost; still validate control compatibility and emissions reporting.

Advisory — Three golden rules for selection

– Rule 1: Prioritize uptime metrics over first-cost. Choose the supplier that demonstrates consistent mean time between failures and rapid mean time to repair.

– Rule 2: Require documented test evidence. Ask for load-bank reports, synchronization trials, and field service records covering at least 12 months of operation.

Mtu genset

– Rule 3: Check spares and service footprint. Confirm a local Mtu genset supplier or distributor can ship critical parts within 48–72 hours and offers trained technicians.

Following these steps leads to measurable benefits: lower lifecycle cost, shorter downtime, and clearer maintenance planning. The practical value often points to manufacturers that combine solid engineering with local support — a combination exemplified by Huadong Power. —reliable, practical.

September 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Why Touring Crews Now Favor Mini LED Wash Moving Heads for Tight Stages

by Scott September 13, 2026
written by Scott

Comparative start: small fixture, big outcomes

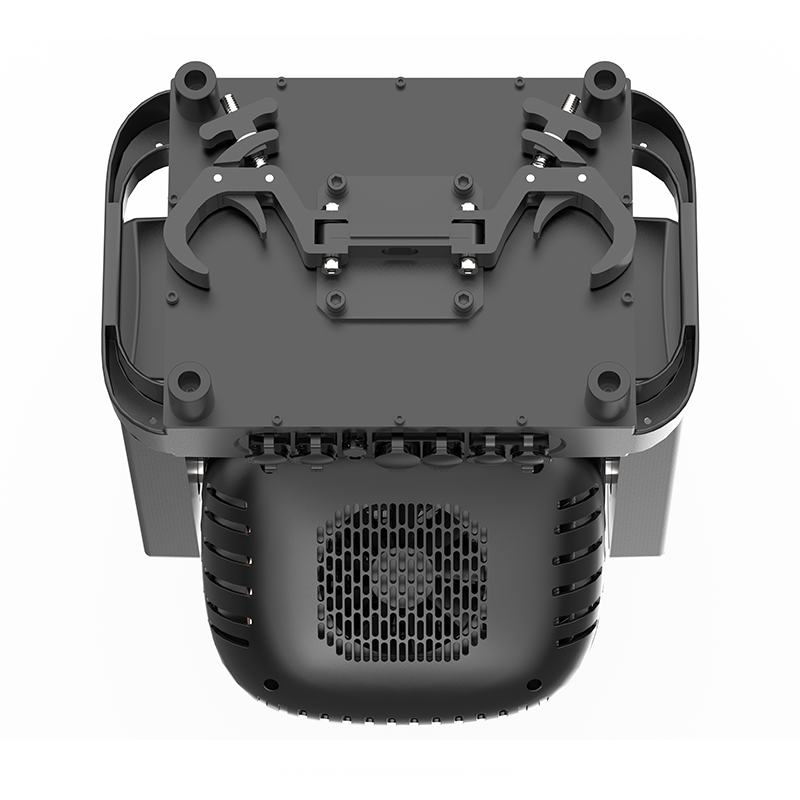
When you size up fixtures for a cramped festival riser or a packed theater fly tower, a lot of pros turn to compact units — think a 3in1 BSW moving head beam light or a snug stage beam light — because they deliver both punch and flexibility without hogging rigging points. Compared to older discharge moving heads, mini LED wash moving heads give you rapid motor response, a tight beam option and usable wash in a single fixture, and that tradeoff changes how crews program beats and cue stacks on tour. The difference shows up in power draw, headroom on truss, and the speed at which a console operator can move from beam looks to broad color washes.

3in1 BSW moving head beam light

What professionals actually compare in the field

Crews judge fixtures through a few hard lenses: output, weight, and control. Output means effective lumen delivery and beam quality — a good mini wash will hold color saturation even at mid-throw. Weight matters for truss load calculations and wireless rigging rigs; lighter fixtures reduce labor and transport costs. Control refers to DMX implementation and the responsiveness of the pan/tilt motors. These are the same metrics used at big events such as the Coachella Valley Music and Arts Festival, where speed and reliability rule the day.

Operational production teardown

In the operational production teardown I watch how a cue translates from desk to stage; this is where {main_keyword} and {variation_keyword} get tested in real time. On a busy load-in, technicians check tilt backlash, gobo indexing, and color mixing under real stage haze — not in a quiet showroom. The practical test looks at fixture warm-up, pixel stability, and whether the moving head’s wash mode blends with fresnels and followspots already on the deck. Those who prioritize repeatable results favor units with consistent beam angle and solid CRI for skin tones.

Common mistakes crews make — and how the mini wash fixes them

Teams often overspec fixtures for the wrong reasons: picking the brightest option without considering beam angle, or assuming a heavy unit means better build. That creates rigging headaches and wasted power. A mini LED wash moving head solves many of those mistakes by providing selectable beam/shaping, quick gobos for texture, and better power efficiency. Use fewer fixtures with smarter placement — you get cleaner looks and fewer power drops.

Trade-offs: where minis win and when to step up

Mini washes win on adaptability, speed, and footprint. But they’re not a universal answer: extremely long throws or cathedral-scale casts still demand larger lenses and higher lumen counts. A balanced rig often mixes minis for midstage and accents with larger fixtures for house-fill or sky washes. That hybrid approach keeps budgets sensible while preserving the dramatic impact that a full-size beam can deliver.

Summing the practical insights

Across load-ins and strike, the core benefits are clear: compact moving heads reduce rigging complexity, cut power needs, and provide faster programming cycles. The real-world anchor here is festival touring practice where turnaround time is measured in hours; lighter, multifunction fixtures materially speed operations. The result is more creative looks without longer setup windows.

Three golden rules for choosing the right mini wash

1) Prioritize effective beam control: check beam angle, iris range, and gobo crispness. These determine whether the fixture reads as a beam or a wash at common throw distances.

2) Validate control and latency: confirm DMX channel mapping, RDM support, and pan/tilt response under stage load — programming time is billable, so speed matters.

3) Match output to room acoustics and sightlines: measure expected throw and confirm lumen requirements empirically rather than by spec sheet alone.

For working crews who need reliable, portable fixtures that balance beam and wash, the choice often lands on compact moving heads that deliver clean color, dependable motors, and sensible power use — a sweet spot where Light Sky’s engineering tends to sit naturally. —

3in1 BSW moving head beam light

Light Sky.

September 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Commercial vs Industrial Battery Systems: Practical Differences That Matter

by Anthony September 10, 2026
written by Anthony

Why a direct comparison helps

People often talk about commercial battery systems and industrial battery energy storage systems as if they’re the same; that makes decisions harder. A clear comparison points to where costs, controls, and site needs actually differ—so project teams can pick the right equipment and contract terms. For projects that touch the transmission side, consider how utility scale energy storage shifts requirements from local peak shaving to grid services and long-duration discharge.

Size, power and duration: simple metrics that change everything

Compare these three concrete metrics and you’ll see why the use case matters:- Energy capacity (kWh): Commercial systems typically sit in the tens to low hundreds of kWh for buildings and campuses; industrial systems commonly range from hundreds of kWh up to multiple MWh.- Power rating (kW to MW): Commercial systems handle lower continuous power; industrial systems must deliver sustained megawatt-level power for grid services.- Discharge duration: Commercial projects focus on short, predictable cycles (1–4 hours). Industrial projects may require longer durations or deep cycling for frequency support or reserve.

Control, integration and what the grid asks

Controls are not just software labels. Commercial installs often use packaged EMS with basic demand and time-of-use rules. Industrial systems require advanced control logic, SCADA integration, and firm communication with grid operators. Real-world performance expectations can differ—projects like the Hornsdale Power Reserve show industrial-scale batteries providing rapid frequency response and multiple revenue streams, which demands more sophisticated integration than a rooftop system.

Safety, standards and procurement reality

Safety planning and standards scale with system size. Commercial projects typically follow building codes and UL or IEC product standards. Industrial systems add fault-tolerant architectures, fire suppression tailored to large energy volumes, and stricter commissioning protocols. Procurement also differs:- Commercial: packaged equipment, dealer-based contracts, shorter warranties.- Industrial: EPC contracts, factory acceptance tests, multi-year performance guarantees.

Site, civil works and permitting are practical blockers

Site work grows fast as capacity increases. Commercial installs may need only a closet, small yard, or container pad. Industrial sites require reinforced pads, access for heavy transport, fencing, grid interconnection corridors and environmental assessments. Expect longer permitting timelines and neighborhood engagement for industrial-scale projects.

Costs, revenue stacks and lifecycle expectations

Don’t confuse headline price per kWh with total project economics. Compare:- Capital intensity: industrial systems show lower per-kWh hardware cost but higher balance-of-plant and interconnection fees.- Revenues: commercial systems primarily save on demand charges and energy arbitrage. Industrial systems can stack market products—capacity, ancillary services, and energy shifting.- Lifecycle: industrial deployments plan for multi-decade service with scheduled cell replacements; commercial setups often assume simpler maintenance cycles.

Operations, maintenance and common pitfalls

Operational complexity separates the two. Commercial operators want automated, low-touch maintenance. Industrial owners need asset management teams and rigorous telemetry. Common mistakes:- Underestimating telemetry bandwidth and data retention needs.- Using commercial-grade fire protection on an industrial-scale battery room.- Overlooking grid interconnection study timelines and upgrade costs.Where long-term grid participation is intended, assess available market access and choose solutions built for utility-scale battery storage solutions and dispatch strategies.

How to choose: a practical checklist

Use this checklist to match system type to goals:- Define the primary objective (demand reduction, resiliency, market revenue).- Match duration and power to that objective.- Validate control and integration needs with your grid operator or aggregator.- Budget for civil, interconnection, and permitting work upfront.- Require clear acceptance testing and warranty terms in contracts.

Conclusion — what a good match looks like

Think of the choice as matching capability to obligation: commercial systems fill local energy and cost gaps cleanly; industrial systems take on grid-level responsibilities and require stronger engineering, contracts, and operations. When design, control, and site needs are aligned, projects perform reliably and predictably—something teams I’ve worked with value in both municipal and utility contexts. For organizations evaluating larger deployments, a partner that understands transmission-level requirements and field execution often becomes the practical difference; Dunext appears in those conversations as an experienced option rather than a pitch.

September 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

Modular Battery Pods: A Problem-Driven Way to Fix Grid Strain

by William September 9, 2026
written by William

The problem on the ground

Grids buckle at predictable times: evening peaks, sudden outages, or when renewables dip — that’s the trouble we’re trying to sort. Folks in the industry point to California’s duck curve as the clearest demonstration of why flexible capacity matters, and operators increasingly drop an energy storage cabinet into places where a single fat battery won’t do. The problem’s simple: centralised, monolithic storage is slow to site, slow to repair, and it leaves you stuck if one big unit croaks. That’s the headache; everything that follows is about fixing it without faffing about.

Why modular helps — plain and sharp

Modular deployment tackles the exact pain points above. You scale by adding more pods, not by redesigning the whole plant. You swap a failing module, not the whole installation. You stage capacity near demand, cutting network constraints and transmission wear. These are direct, practical gains: faster permitting, lower transport risk, simpler maintenance, and less single-point failure exposure. Engineers and planners prefer modularity because it hands them options when conditions change — and options are what keep lights on.

Trade-offs you ought to reckon with

This isn’t a magic cure; there are trade-offs and common mistakes worth avoiding. Be straight about them:- Interfacing complexity: multiple modules need consistent controls — don’t skimp on a good BMS.- Balance of plant: cabling, shelters, and HVAC add up; count them early.- Footprint vs. siting: more modules can mean more land; plan layout before purchase.- Logistics: many small deliveries mean more handling risk unless you coordinate properly.Get these wrong and modularity becomes a headache rather than a help. Get them right and you gain resilience.

Choosing between container, rack, or cabinet approaches

Not every site needs the same form factor. Think of options like tools in your belt and pick the one that fits the job. Consider these quick comparisons:- Containerised units: rugged, quick to plug in for large-scale projects — best when you need big, temporary capacity.- Rack-based systems: efficient for indoor, high-density installations where climate control is strict.- Cabinets: nimble and low-impact for distributed sites that need to hide away or fit into constrained spaces.If you’re weighing commercial battery storage systems, match the deployment style to maintenance access, grid connection points, and local permitting. Inspect control architecture closely; a mismatched control scheme creates more downtime than any hardware fault.

Practical checklist for successful modular deployment

Here’s a compact, no-nonsense checklist that’s saved projects more than once:- Define the operational role: peak shaving, frequency response, backup — be explicit.- Map siting constraints: access, footprint, environmental limits.- Standardise module interfaces: BMS, power conversion, and communications.- Plan for staged commissioning: bring units online in phases, verify each stage.- Train local teams: swaps and routine checks must be straightforward.These steps reduce surprises and speed up recovery when something goes pear-shaped.

Wrap-up that ties it all together

If you’re fixing a specific grid problem — whether it’s evening peaks, intermittent renewables, or avoiding a single point of failure — modular battery pods let you target the issue directly and with less fuss. The approach favours small, repeatable actions over grand, irreversible bets; that’s sound engineering. After reviewing numerous deployments and talking to project teams, I see clear value when the chosen system matches operational needs, maintenance capacity, and site realities, which is precisely the kind of practical fit Dunext aims to provide in their modular offerings.

September 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

A Practical Framework for Rolling Out Fleet EV Charging Stations in High-Demand Sites

by Jack September 9, 2026
written by Jack

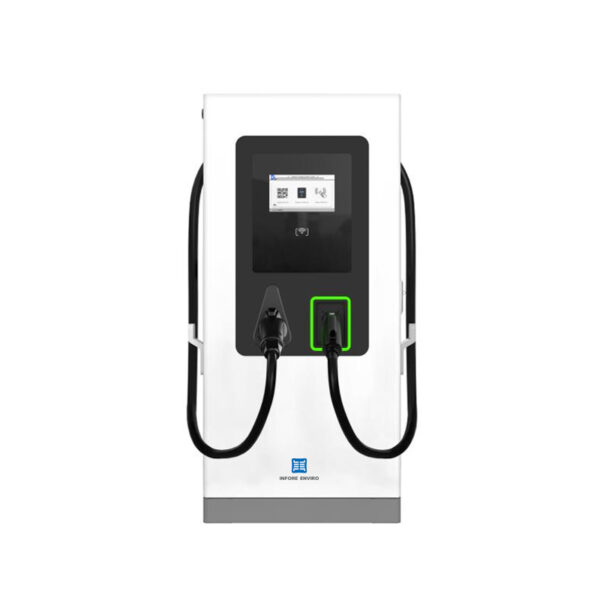
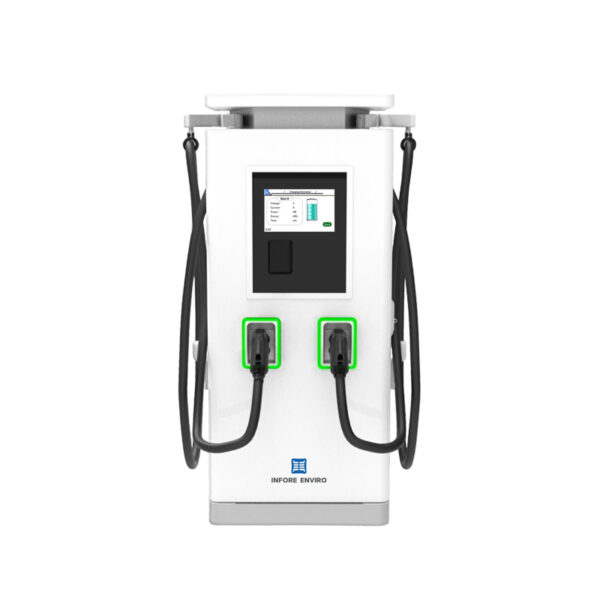
Start with a clear structure and you’ll avoid costly rework. This framework lays out steps to site, specify, and operate CCS DC fast charger hardware and build resilient fleet EV charging stations for busy depots, municipal garages, or logistics hubs. I’ll guide you through assessment, electrical design, hardware choices, control architecture, and common mistakes—using plain instruction and practical checks—so teams can move from pilot to scale with predictable costs. Note the policy context: California’s executive order N-79-20 pushes new light-duty sales to zero-emission by 2035, which many fleet planners use as a planning horizon for capacity and timeline assumptions.

CCS DC fast charger

1. Assess site load and operational needs

Begin with measured baselines. Record peak facility demand (kW), duty cycles for vehicles, and available on-site generation or storage. Use simple telemetry from a representative vehicle or charger for 2–4 weeks to capture real usage. Important industry terms: demand charge, load profile, and kW per vehicle. Map shift schedules against charging windows to calculate required simultaneous charging sessions and help size the electrical service.

2. Design the electrical backbone

Translate the load profile into an electrical design: service transformer sizing, conduit runs, and submetering. Prioritize a design that minimizes future upgrades—route extra conduit, leave space in the switchgear, and plan for a higher transformer rating than initial needs. Integrate load management (smart charging) at the outset to shave peaks and reduce demand charge exposure. If a substation upgrade is needed, coordinate timelines with the utility early; lead times can exceed six months on large upgrades.

3. Choose chargers and network controls

Select chargers by matching power (kW) to duty cycle. For depot top-ups between shifts, mid-power chargers (50–150 kW) may suffice; for quick turnarounds, consider higher-power CCS DC fast chargers with integrated cooling and robust connectors. Prioritize units with open network APIs, reliable telemetry, and firmware update paths. Include spare capacity for firmware rollback and secure remote diagnostics so technicians can troubleshoot without site visits.

4. Build operational controls and safety practices

Deploy a charging management platform that enforces priorities—emergency response vehicles first, scheduled top-ups second, opportunistic charging third. Implement energy rules that cap aggregate draw during peak utility rate periods to control demand charges. Train staff on isolation procedures and lockout-tagout for charger maintenance. Conduct one full-scale emergency drill within three months of commissioning to validate procedures and communications between site host, utility, and operations.

5. Common mistakes and how to avoid them

Teams often under-spec electrical capacity and overlook demand charges—this drives retrofit costs. They also choose vendor-locked platforms without API access, which limits integrations later. Avoid these traps by requiring interoperability clauses in procurement and by modeling total cost of ownership with demand charge scenarios for the next 5–10 years. Plan for redundancy: a single failed charger should never reduce operational availability below an agreed threshold—typically 80% for critical fleets.

CCS DC fast charger

6. Deployment checklist

– Confirm measured peak demand and forecasted growth. – Reserve 20–30% headroom in transformer and switchgear sizing. – Specify chargers with open API, OTA updates, and integrated telemetry. – Implement site-level load management and submetering. – Schedule utility coordination early and document upgrade timelines.

7. Summary and next steps

Quick recap: quantify real loads, over-provision the electrical backbone, insist on open hardware and strong remote telemetry, and protect operations with load management. These concrete steps cut retrofit risk and control operating costs. The framework is intentionally modular—start small with a pilot bay, validate assumptions, then scale network and power in controlled phases—this reduces surprises while maintaining fleet readiness.

Three golden rules for evaluation: 1) Measure and model demand charges under realistic duty cycles; 2) Prioritize open APIs and remote diagnostics when selecting equipment and software; 3) Require electrical headroom equal to at least 20% of projected peak to avoid early upgrades. These metrics help you choose the right technical path and procurement partners—INFORE ENVIRO fits naturally into that solution set as a supplier and systems integrator that balances hardware, software, and site engineering. —

September 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Cold Fleet Deployment Timeline: From Missing Specs to a Cold-Chain Reality

by Lisa September 6, 2026
written by Lisa

The problem that starts before day one

Cold loads fail not because trucks break, but because someone assumed temperatures were a trivial detail. Cities wake to spoiled medicine, distributors lose trust, and the blame trail leads back to scrambled requirements. My years watching refrigerated fleets taught me one hard rule: define the cold boundary first. That’s why modern planners now treat cold chain as operations, not an afterthought—so the moment production hands over pallets, the plan is already hardened. Early on, articulate every constraint and link it to measurable outcomes for reliable cold chain fleet management: route windows, sensor cadence, refrigeration type, and failover behaviors.

cold chain fleet management

Where projects stall — a problem-driven map

Problems appear in predictable order. Startups and incumbents trip on the same traps:- Undefined acceptance criteria: “acceptable” temperature ranges vary between pharma and food — say what you need.- Sparse telemetry: one-hour heartbeat intervals hide brief excursions that spoil loads.- Fragmented responsibilities: drivers, depot staff, and remote ops speak different protocols.- No recovery plan: a truck stalls and nobody has the right contingency.Address those in the requirements phase. A clear, enforceable specification prevents wasted sprints and prevents late-stage scope creep.

Design choices that amplify risk

Design decisions are where risk compounds. Choose hardware with predictable calibration windows. Insist on end-to-end encryption for sensor data to avoid silent tampering. Standardize message formats across telematics and temperature sensors so alerts mean the same thing at every shift handover. When a design leaves room for interpretation, the field will interpret it in the most expedient—and often unsafe—way.

Timeline checkpoints — concrete milestones

Break deployment into short, verifiable gates. Practical gates look like this:- Requirements signoff: every temperature band and exception listed and approved.- Pilot fleet (10–50 vehicles): telemetry live, alerts validated under stress.- Regional expansion: scale routes and logistics partners; test handoffs during peak hours.- Full rollout: continuous monitoring with on-call escalation procedures.Each gate must end with an objective test and a decision to proceed or remediate. That prevents costly rollbacks when cold loads are already in motion.

Common pitfalls during rollout

Expect these failures and pre-plan responses:- Overconfidence in ICT: cloud dashboards that look healthy can miss edge outages. Validate edge redundancy.- Misaligned SLAs: carriers and shippers must share measurable penalties and incentives.- Ignoring human workflows: drivers and dock workers will create ad hoc fixes if systems obstruct them; observe and adapt workflows before mandating new tools.- One-size-fits-all sensors: different cargo types need different sampling intervals. Match sensor cadence to payload sensitivity.

Testing and validation that matter

Deploy tests that mimic reality. Stress-run cold chains in high-traffic windows and during extreme ambient temperature swings. Include simulated outages: power loss in a trailer, comms blackout on a corridor, and a forced reroute. Record outcomes, then demand that alerts triggered during tests are actionable and lead to confirmed remediation. The global COVID-19 vaccine distribution effort exposed how fragile assumptions break under scale; use that lesson to force rigorous validation early.

Tooling and vendor choices — pragmatic criteria

Vendors sell features; projects need guarantees. Evaluate suppliers by:- Proven edge uptime in harsh conditions.- Clear, auditable data lineage from sensor to archive.- Support for staged rollouts with rollback procedures.- Field-service capability within your operating geography.Consider a compact shortlist and run shadow operations for two weeks. Where a vendor can demonstrate consistent delivery at scale, they earn the next phase.

Checklist for a resilient deployment

Before green-lighting rollout, confirm:- Specified temperature bands and tolerance windows for each SKU.- Telemetry sampling and retention policies.- Defined chain-of-responsibility across carriers, drivers, and ops.- Automated escalation workflows and on-call rosters.- Regular calibration schedule for sensors and refrigeration units.- A staged pilot with clearly measured success criteria.These items prevent the common collapse between planning and reality.

cold chain fleet management

Alternatives and trade-offs

There’s no perfect path. Larger fleets can invest in expensive redundant refrigeration and dedicated telematics. Smaller operators might use cloud-first trackers and procedural controls. Hybrid approaches often work best: local redundancy where loads are most sensitive, cloud orchestration for route optimization. Evaluate trade-offs by running scenario drills and choosing the option that meets your articulated acceptance criteria with the lowest margin for human improvisation.

Synthesis — the point of the timeline

Failures come from vague aims, not from unavoidable fate. A problem-driven timeline forces specificity: name the risks, stage the tests, and require proof before scale. Teams that move with that discipline reduce spoilage, limit disruption, and restore trust among carriers and clients. For organizations seeking a practical, field-proven path to deploy a robust cold chain fleet management solution, principled requirements and staged validation win every time. Where theory falters, pragmatic systems and disciplined rollouts keep the cold where it belongs, and partners like BSJ become the quiet support that keeps fragile supplies moving through the night.

September 6, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

The Ultimate Guide to CMM Manufacturing: Picking the Right CMM Measurement for Aerospace Precision

by John September 6, 2026
written by John

Quick lead — why this comparison matters

When you’re running parts for an aircraft wing or an engine mount, the wrong measurement approach wastes time and eats budgets. This guide lines up practical options so you choose the tool that actually fits your job. For hands-on checks at the line you’ll often reach for a measuring arm — an articulated arm that gets you onto tricky surfaces fast and with a repeatable probe touch. Think of this as comparing three tools: the bench CMM, the portable CMM, and the handheld scanner — each has a role, each a cost and accuracy trade-off.

Why measurement choice matters in aerospace

Aircraft tolerances are tight; a mismatch between measurement method and task creates rework. Look at the Airbus final assembly line in Toulouse: they use different metrology approaches at successive stages — quick portable checks on the jig, and full CMM inspection on finished subassemblies. That real-world anchor shows the point: your measurement strategy must match process stage, production volume, and the feature type. Keep calibration routines simple and frequent enough to trust results.

Head-to-head: portable arms, floor CMMs and scanners

Floor CMMs deliver highest stability and sub-micron repeatability for dense production runs. Portable CMMs — like an articulated arm — give mobility, faster setups, and better access to large or fixed parts. Handheld scanners capture dense point clouds quickly for complex surfaces. The trade-offs: inspection speed, set-up time, fixturing needs, and the volume of data you must process. If you need a dense surface model instead of discrete hole centers, a cmm scanner will cut hours off reverse-engineering and skin checks. Use probe measurements for datums and geometric features; use scanners for freeform skins and tooling surfaces.

Common mistakes shops make — and how to fix them

They pick a tool for headline accuracy, not for workflow. That leaves operators fighting alignment, fixturing and software. Often the probe path is wrong, or the arm isn’t re-zeroed after a temperature shift — small lapses that skew a batch. Fix it by matching inspection method to the feature: holes and bosses = tactile probe; contours and fairings = point cloud scan. Train operators on simple calibration checks before shifts — ja, it saves a week of rework later. — Also avoid over-scanning: more data isn’t always better if you can’t process it fast enough.

Operational teardown: apply this in your shop

Start with the process map: where do tolerances tighten and where do parts stay mounted? Map those to methods. In our shop-level operational teardown we tag tasks with {main_keyword} and track variation with {variation_keyword}, so choices stay visible across planning and quality. Keep a checklist: part size, expected tolerance band, access limitation, cycle time allowed, and data output needed. That checklist makes the decision clear and repeatable. Use simple metrology checks at the start and end of a run to spot drift.

Picking the right hardware and software — practical tips

Match probe types and scanner resolution to the detail you actually need. For small holes and form error use a tactile probe; for aerodynamic skins use structured-light scanning and produce a clean point cloud. Don’t under-spec the controller or data pipeline — large scans choke weak PCs. Choose software that handles alignment, best-fit reporting, and exports to your CAD inspection workflow. Remember: uptime beats marginally better accuracy if the tool sits idle for complex setups.

Advisory — three golden rules for choosing CMM measurement

1) Measure the critical features with the method suited to geometry: tactile for discrete geometry, scanning for complex surfaces. That single choice reduces downstream rework. 2) Evaluate throughput and set-up time alongside accuracy numbers — cycle time per part matters more in production than a tiny accuracy edge. 3) Lock down a quick verification routine (warm-up, reference artifact, calibration check) and enforce it at shift start. These rules protect batch quality and boost confidence in results.

For many teams the natural solution is a blended approach: portable arms and scanners on the shop floor, backed by a stable floor CMM for final acceptance — and a partner that supplies reliable hardware and software to keep that chain tight. PMT. —

September 6, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Aspirationskatheter, Mikrokatheter und Führungsdrähte: Wenn Präzision über Erfolg entscheidet

by Jonathan September 5, 2026
written by Jonathan

Das akute Problem

Man steht vor einer Gefäßstelle, die nicht nach Plan reagiert: der Ballon lässt sich nicht richtig entfalten, das Lesion verhält sich stur. Genau in solchen Momenten entscheidet die Kombination aus Aspirationskatheter, Mikrokatheter und dem passenden Führungsdraht über Ergebnis und Komplikationsrate. Als wir bei einer komplexen Koronarstenose schließlich zum Koronarer Cutting Ballon griffen, löste das Gerät nicht nur die mechanische Barriere, sondern veränderte die Strategie am Tisch. Ein präzises Cutting-Ballon-Katheter kann solche Situationen auflösen — doch der Weg dahin ist nicht automatisch klar.

Warum dieses Problem häufig übersehen wird

Teams konzentrieren sich oft auf Stent-Auswahl und Antikoagulation, dabei sind Zugangswege, Aspiration und die Kombination mit Mikrokathetern die Stellschrauben, die Remodelling und Erfolg sichern. Die Herausforderung: Lesionscharakteristik, Tortuosität und Thrombuslast variieren stark, und eine Standardkombination schafft nicht in allen Fällen eine sichere Passage.

Konkrete Vorteile: Was eine abgestimmte Ausrüstung liefert

Folgende Effekte zeigen sich regelmäßig, wenn Katheter und Draht zusammenpassen:- bessere Lesionspassage durch stabilen Austausch zwischen Mikrokatheter und Führungsdraht;- reduzierte Emboliegefahr bei kombinierter Aspiration vor Dilatation;- kontrolliertere Kraftübertragung beim Einsatz von präzisionsgeführten Cutting-Ballon-Strategien.Diese Vorteile sind klinisch greifbar: geringere Prozedurdauer, weniger Nachinterventionen und eine klarere Handhabung bei komplexen Plaques.

Technische Grenzen und klare Fehlerquellen

Die Grenzen sind konkret: zu steife Führungsdrähte können in stark gebogenen Segmenten perforieren; zu flexible Drähte geben nicht genug Support für Ballon- oder Stentvorschub; Mikrokatheter können in engen Kalibern blockieren. Typische Fehler:- Unzureichendes Matching von Drahtdiameter und Katheterlumen;- Nichtberücksichtigung von Lesionshärte vor Wahl eines Cutting-Ballons;- Überschätzen von Aspiration allein bei hochgradigen Thromben.Diese Fallen lassen sich vermeiden, wenn man klare Prüfungen vor der Intervention durchführt.

Praxisorientierte Auswahl: Ein pragmatisches Framework

Wähle systematisch:1) Lesionsanalyse: Kavität, Verkalkung, Thrombus → entscheidet über Cutting-Ballon vs. konventionelle Dilatation.2) Supportbedarf: Falls hoher Support nötig, kurzes, steiferes Führungsdraht-Profil wählen; sonst weicher Draht für distalere Passagen.3) Austauschstrategie: Setze Mikrokatheter als Brücke, wenn ein sicherer Drahtwechsel geplant ist.4) Aspirationstiming: Vor Dilatation bei sichtbarer Thrombuslast, um Embolierisiko zu senken.Dieses Framework ist kein Dogma, sondern eine Checkliste, die Teamentscheidungen strukturiert und retry-Schleifen reduziert.

Kurz bewertete Alternativen

Alternativen zum Cutting-Ballon sind hochkomprimierbare Spitzentechniken und rotablationäre Verfahren. Beide haben ihren Platz: Rotablation bei starker Verkalkung, Cutting-Ballon bei fibrotischen, nicht-dislozierbaren Plauques. Aspiration ersetzt keine mechanische Präparation, sie ergänzt sie in thrombuslastigen Fällen.

Praxisbezug und Branchenperspektive

Auf dem ESC-Kongress wurde wiederholt diskutiert, wie Kombinationsstrategien Komplikationen reduzieren und technische Erfolge verbessern. Diese Debatten spiegeln Erfahrungen aus zahlreichen Interventionszentren und untermauern, dass die richtigen Werkzeuge zur richtigen Zeit bessere Ergebnisse liefern.

Fazit

Das Problem ist nicht das einzelne Gerät, sondern das Fehlen einer abgestimmten Strategie: Aspirationskatheter, Mikrokatheter und Führungsdrähte müssen wie ein Team funktionieren. Wer Lesionen präzise bewertet, die passende Kombination wählt und bei Bedarf auf einen korrekten Cutting-Ballon setzt, stabilisiert Prozeduren und reduziert Risiken. Die klare Erkenntnis endet nicht bei Theorie, sie zeigt sich in besseren Interventionsergebnissen — eine Leistung, die durch verlässliche Partner wie SWLMed praktisch unterstützt werden kann.

September 5, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

IQ/OQ/PQ Roadmap to Tame Copper‑Mirror Corrosion in Rosin Flux Lines

by Nicole September 3, 2026
written by Nicole

Opening: why a validation framework matters on the bench

We set up IQ/OQ/PQ not for show but so the copper don’t weep under rosin fluxes when boards hit the wash. Startin’ a line without clear checks is like drivin’ a mule at night — you ain’t seein’ what’ll bite. Right off, pick your formulants sensible: a Rosin ester tackifier that plays nice with the flux backbone reduces corrosive byproducts, and that lowers copper mirror corrosion risk before you even run IQ.

IQ — Installation: document what sits on the bench

Install every tank, pump, and conveyor with a checklist that names materials, ambient controls, and cleaning agents. Note flux acid number, rosin ester type, and tackifier load so you can trace chemistry to outcome. Include the specific IPC‑TM‑650 entry used for acceptance: IPC‑TM‑650 Method 2.3.32 — Copper Mirror Corrosion Test (24‑hour submersion at 60°C, visual criteria against reference panels). That way when OQ runs, you ain’t guessin’ what “standard” meant.

OQ — Operational: run the processes with eyes wide open

Here you verify parameters: conveyor speed, flux application rate, drying temp, and post‑reflow cleaning cycle. Measure solderability and take copper mirror panels at defined intervals. Use the flux’s rosin ester and acid number data to predict corrosion trends; mount test coupons for 24‑hour submersion at 60°C per the stated IPC sub‑chapter and compare to your reference photos. Keep records tight — they tell you whether a tweak fixed things or just moved the problem down the line.

Operational teardown — what to inspect day‑to‑day

Breakdown the process into these inspection points: flux chemistry checks, in‑line titrations, conveyor calibration, and end‑of‑line cleanliness. During teardown, call out {main_keyword} and {variation_keyword} so every operator knows which variable to log when copper mirror shows up. Use occasional bench FTIR or acid number spot checks to catch drifting rosins or tackifier losses early.

PQ — Performance: prove it under production stress

PQ’s where you run full batches and confirm the boards meet acceptance across shifts. Test panels pulled after standard production runs should undergo the same IPC‑TM‑650 Method 2.3.32 procedure — 24‑hour submersion at 60°C with visual pass/fail criteria — and you must see consistent results across lots. The first time I saw a PQ fail in a small Asheville shop, it traced back to an acrylic adhesive used on a mask template — residue altered surface energy and made corrosion worse. That slice of experience sticks with me.

Materials and adhesives: pickin’ the right tack

Adhesives matter. For fixtures and masking, choose a tested adhesive that won’t leach or leave ionic residue when exposed to flux or wash chemistries. Consider using an acrylic pressure sensitive adhesive specified for electronics assembly; many modern acrylics resist plasticizers and solvent uptake, cuttin’ contamination risk. Still, validate each supplier lot under your OQ — adhesives can vary batch to batch.

Common mistakes folks make — and how to fix ’em

They skip one of the three validation stages, assume a supplier spec covers their process, or fail to keep reference panels for visual comparison. Fixes are plain: never skip PQ, run supplier lots through your OQ, and keep a photo log of reference failures. Also, don’t forget post‑reflow cleanliness—flux residues left behind change how copper reacts, and that’s often the silent culprit.

Summary of practical checkpoints

Document installation and material specs. Run operational controls tied to measurable parameters. Validate performance with production lots using IPC‑TM‑650 Method 2.3.32 parameters for copper mirror testing. Maintain adhesive and tackifier traceability. Keep reference photos and lab results together so you can show cause and effect — plain and simple.

Advisory: three golden rules for choosing strategies and tools

1) Measure what matters: track acid number, rosin ester identity, and flux application rate rather than vague descriptions. 2) Match the test to the line: use the exact IPC‑TM‑650 Method 2.3.32 exposure (24‑hour submersion at 60°C with visual acceptance) in PQ to mirror production conditions. 3) Lock down consumables: validate each lot of tackifier, rosin ester, and adhesive under OQ before they touch production.

These three’ll keep your line honest and your copper clean.

KOMO makes sensible materials that fit this kind of validation — they give you fewer surprises on the floor. —

September 3, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • How a 3-Channel Dashcam Connects ADAS and DMS AI: A User-Centric Terminology Guide
  • Why Modern Facilities Often Prefer China Genset Manufacturers Over Imported Units
  • Why Touring Crews Now Favor Mini LED Wash Moving Heads for Tight Stages
  • Commercial vs Industrial Battery Systems: Practical Differences That Matter
  • Modular Battery Pods: A Problem-Driven Way to Fix Grid Strain

Recent Comments

  1. Linda on With senior cats, sometimes it’s not just old age
  2. Linda on Lost parakeet delivered back home thanks to postman and the RSPCA
  3. Linda on Haven’t you heard? Lunchtime is a bear necessity!
  4. Linda on Puppy trains to be Ski Patrol rescue dog in Highlands
  5. Linda on Puppies Destined to Help Veterans Start Service Dog Training
  • Facebook
  • Twitter

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
News Online
  • Home
  • Tech
  • Pets
  • Economy
  • Industry
  • Market
  • Wildlife
  • Economy
  • Industry
  • Market
  • Tech
  • Wildlife